Research Themes
Micro EDM |
Micro Cutting |
Micro Grinding |
Micro USM |
Micro ECM |
Micro Shearing |
Hybrid Micromachining
Micro USM (Ultrasonic Machining)
Ultrasonic Machining of Micropins
The fabrication of convex shapes by micro USM was performed[cite: 12]. A cemented tungsten carbide micropin of 5 µm diameter was successfully machined[cite: 12]. The machined surface can be smooth and glossy[cite: 12].
Paper (Journal of the Japan Society for Abrasive Technology, Vol.50, No.11, 2006, pp.649-653)[cite: 12]
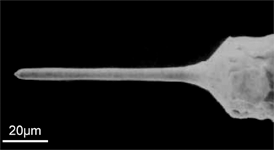
Fabricated micropin of 5 µm diameter
Microultrasonic Machining by the Application of Workpiece Vibration
In order to obtain high-precision tool rotation, a spindle mechanism employed in micro-EDM machines was introduced[cite: 12]. Since the mechanism does not allow the vibration of tools, the workpiece was vibrated[cite: 12]. As a result, microholes of 5 µm diameter were successfully drilled[cite: 12]. These holes have the smallest reported diameter for holes drilled by USM[cite: 12].
Paper Paper (KIT only) (Annals of the CIRP, Vol.48, No.1, 1999, pp.131-134)[cite: 12]
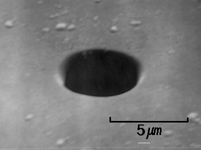
Drilled microhole of 5 µm diameter
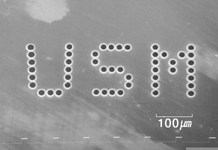
48 holes drilled with single PCD tool
Application of USM to Micromachining by On-The-Machine Tool Fabrication
A technique of micro USM by applying on-the-machine tool fabrication by EDM was proposed[cite: 12]. Microholes of 20 µm diameter were drilled in silicon[cite: 12]. Noncircular microholes were also fabricated[cite: 12].
Paper (International Journal of Electrical Machining, No.2, 1997, pp.31-36)[cite: 12]
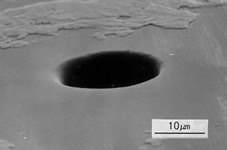
Microhole of 20 µm diameter
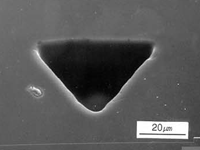
Triangular microhole
Microultrasonic Machining Using Multitools
Micro USM with a single tool is time-consuming[cite: 12]. In this study, multitools were fabricated and then used in the machining of arrays of microholes[cite: 12]. The drilling time per hole was greatly reduced[cite: 12].
Paper (Proceedings of The 7th International Conference on Progress of Machining Technology, 2004, pp.297-301)[cite: 12]

Multitool
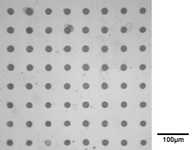
Arrays of microholes drilled
Study on Material Removal Mechanism in Microultrasonic Machining
No sharp edges caused by brittle fracture are observed on surfaces processed by micro USM[cite: 12]. It is probable that the material removal mechanism in micro USM is based on ductile fracture, not on brittle fracture as in conventional USM[cite: 12].
Paper (Proceedings of The 5th International Conference on Progress of Machining Technology, 2000, pp.739-743)[cite: 12]
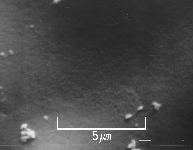
Surface processed by micro USM
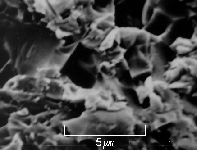
Surface processed by conventional USM